Is Machine Vision Better Than Manual Checks for Decorative Panel Finishes?





Machine vision is often better than manual inspection for repeatable, measurable defects on a stable production line, but it is not automatically better at judging decorative appearance. A camera system can consistently flag scratches, spots, or coating gaps when lighting and acceptance limits are controlled. Human inspectors remain valuable when deciding whether a grain pattern looks unnatural, a texture feels wrong, or a subtle finish difference is acceptable.
On a decorative panel line, that distinction affects rejected shipments, unnecessary rework, and customer complaints. A mark visible under inspection lights may disappear in normal use, while gloss variation missed during a quick check can become obvious when panels are installed together. Is machine vision better than manual inspection for decorative panel finishes? The practical answer depends on the defect, viewing conditions, production mix, and whether “acceptable appearance” has been defined clearly enough to measure.
Start with the defect, not the inspection equipment
Decorative panels include laminated boards, printed surfaces, coated metal, veneered panels, and textured finishes. These surfaces do not present the same inspection problem. A uniform matte coating may allow straightforward detection of dark spots, while a woodgrain print can conceal scratches and produce legitimate features that resemble defects.
Before comparing cameras with inspectors, separate finish problems into three groups:
- Discrete defects: scratches, pinholes, particles, chips, coating voids, and localized stains. Their size, location, and contrast can often be described objectively.
- Surface consistency problems: color drift, uneven gloss, streaking, and texture variation. These require controlled measurement conditions and suitable reference samples.
- Aesthetic judgments: whether grain looks convincing, adjacent panels coordinate, or a variation disrupts the intended design. These may remain partly subjective even after inspection rules are documented.
A system that detects particles well is not necessarily capable of measuring gloss or approving decorative character. Asking one camera and one lighting arrangement to solve every category is a common source of disappointing results.
Where each approach performs better
The distinction is not simply “objective machines versus subjective people.” Software thresholds reflect human decisions about acceptability. Manual checks can also be disciplined and repeatable when inspectors use boundary samples, controlled lighting, and clear defect rules.
Lighting can decide the result before software does
A camera only evaluates the information captured in its images. If a scratch produces no visible contrast, a more sophisticated algorithm cannot reliably recover it. Decorative finishes make this particularly important because reflections change with surface angle, panel movement, and light position.
Diffuse lighting can reduce glare and help reveal color or printed-pattern differences. Low-angle illumination can emphasize fine scratches and raised contamination. Specular arrangements can expose changes in reflected appearance, but may also make harmless surface variation look severe. Some applications need multiple views or lighting modes rather than one inspection image.
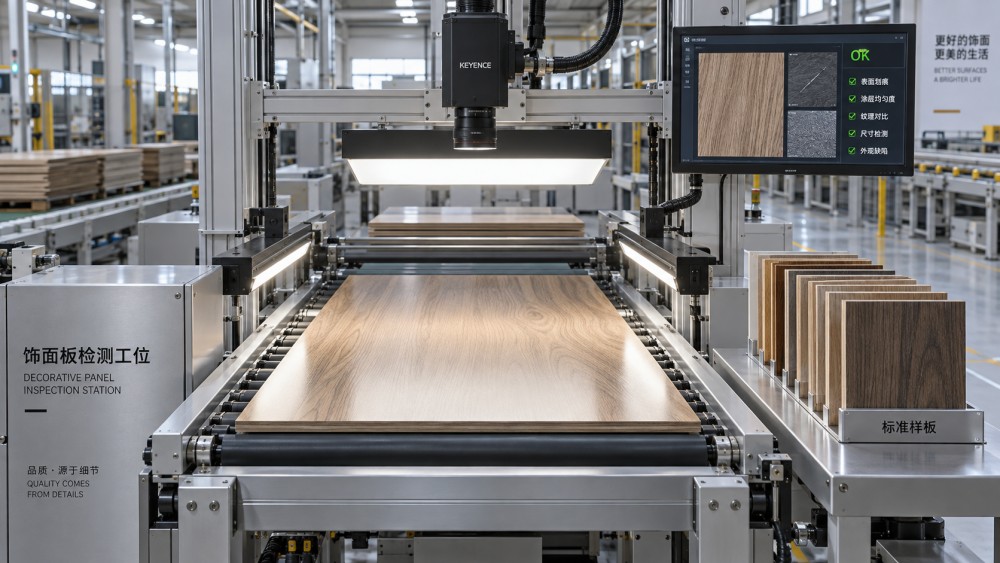
Panel flatness and position matter too. A slightly bowed glossy panel can redirect reflections and resemble a finish defect. Vibration, inconsistent conveyor height, or changing distance from the camera can alter the image even when the coating is unchanged. Enclosing the station against ambient light, stabilizing panel presentation, and maintaining lenses and lights are part of the inspection process.
Color and gloss need separate acceptance logic
Color inspection should distinguish between detecting a visible change and measuring color against an agreed tolerance. Camera-based color measurement requires appropriate calibration, stable illumination, and validation against a suitable reference method. Some applications are better served by a spectrophotometer or an integrated color measurement instrument.
Likewise, brightness in an image is not a direct substitute for gloss measurement. The chosen geometry must match the finish and inspection objective. Where contractual limits specify color or gloss measurements, automated results should be checked against those requirements rather than accepted because a dashboard displays a numerical score.
Manual inspection also needs controlled conditions. Moving a panel between daylight, warehouse lighting, and a desk lamp can change the apparent result. Panels intended to sit next to one another may need comparative review in a viewing arrangement representative of installation.
Throughput is useful only if the decisions remain reliable
Machine vision can inspect continuously without fatigue, but nominal processing speed does not establish detection capability. The smallest relevant defect must occupy enough image detail to be distinguished from noise and surface texture. Exposure, panel speed, camera arrangement, and illumination must work together to avoid motion blur and missed areas.
Large panels may require line-scan imaging, multiple cameras, or overlapping views. Edges, corners, and recessed features can need separate inspection positions. A proposal covering only the main face should not be treated as complete finish inspection if edge damage is a significant rejection reason.
Manual inspection has different constraints. At a fast conveyor pace, an inspector may have time to see obvious damage but not subtle surface inconsistency. Increasing staffing can improve coverage, yet introduces handoffs and differences in judgment. A slower, well-defined manual station may outperform a poorly configured automated one.
Compare both approaches using missed defects and false rejects, not inspection speed alone. Missed defects can reach customers; false rejects can send acceptable panels into rework, scrap, or unnecessary review. A camera system that flags large amounts of normal grain variation may shift the workload rather than reduce it.
Define “acceptable” before running a supplier demonstration
The most useful preparation is an acceptance specification tied to real finish problems. “No visible defects” leaves too much room for disagreement. Define relevant defect size, visibility, location, frequency, and inspection conditions where these can be established reasonably.
Location can change severity. A small mark near a concealed edge may be acceptable while the same mark in a prominent area is not. Batch matching can also matter: panels that pass individually may still look inconsistent when assembled together.
Reference samples should include accepted variation, clear rejects, and borderline examples. Keep them identified and protected against damage or fading. For natural-looking finishes, include legitimate pattern diversity so that neither operators nor software learn an unrealistically narrow definition of a good panel.
- Agree on the reference decisions. Have quality and production personnel resolve disputed samples before using them to judge either inspection method.
- Test representative material. Include relevant finishes, different batches, edge conditions, and defects that are difficult to see—not just demonstration samples with obvious damage.
- Separate development from evaluation. Assess performance on samples not used to tune rules or train a model. Include normal production variation.
- Run at production conditions. Check actual speed, positioning changes, ambient-light control, and the reject mechanism.
- Review errors by category. Record missed defects and false rejects separately for scratches, spots, color, texture, and other relevant problems.
Aggregate accuracy can hide weaknesses. A trial containing mostly good panels may produce an impressive overall result while missing a commercially important defect class. Performance should therefore be examined by defect type and severity, with enough examples to make the assessment meaningful.
The implementation cost extends beyond cameras
Machine vision costs include optics, lighting, mounting, guarding, software, integration, commissioning, reference measurement, and operator training. Depending on the line, automated rejection and image storage may add further requirements. Maintenance must cover dirty optics, aging illumination, calibration checks, and changes to product recipes.
Frequent finish changes can increase engineering effort. A setup validated for a smooth, light-colored panel may not transfer directly to a dark embossed surface. Rule-based methods and trained models both need reassessment when materials, patterns, or process conditions move outside their validated range.
Manual inspection costs are not limited to wages either. Include training, supervision, breaks, lighting stations, inconsistent decisions, and downstream reinspection. Compare total cost at the required quality level, rather than camera investment against the current staffing bill alone.
Procurement specifications should state what the supplier must demonstrate: inspected areas, finish families, defect categories, operating speed, changeover procedure, and access to rejected images. Clarify who maintains inspection recipes and how software changes will be validated. These details help distinguish a production-ready system from a successful laboratory demonstration.
A hybrid process often resolves the difficult cases
Automation is a strong fit when production volume is steady, defects are visually measurable, and the surface range is manageable. Manual inspection may remain more practical for low-volume custom finishes, frequent design changes, or acceptance decisions dominated by aesthetic judgment.
A hybrid arrangement gives each method a defined role. Machine vision screens for validated defect classes and records suspect locations. A trained reviewer handles borderline images or selected physical panels, while periodic manual audits check whether apparently acceptable production contains missed problems.
Image review alone is not always enough. When acceptance depends on reflected appearance, texture, or comparison between panels, the reviewer may need the actual material under agreed lighting. The process should specify how uncertain panels are held and released rather than allowing them to disappear into an informal recheck queue.
Feedback should be controlled. Adding every rejected image to a training set without confirming its label can reinforce incorrect decisions. Changes to thresholds or models should be tested before release, with records linking decisions to the inspection version in use.
The strongest reason to choose machine vision is demonstrated improvement in detection and consistency under actual production conditions. Retain manual judgment wherever the automated method has not proved reliable, and expand automation by validated defect category—not by assuming that successful scratch detection means the entire decorative finish can now be approved automatically.
Industries
Related News
- 00
0000-00
US Treasury Extends Russia Oil Sanctions Waiver by 30 Days - 00
0000-00
International Logistics Solutions for Heavy Machinery: Cost Risks and Route Planning in 2026 - 00
0000-00
Energy-saving home improvement ideas with faster payback - 00
0000-00
10 Smart Home Decoration Ideas to Make Small Rooms Look Bigger and Brighter - 00
0000-00
Shenyang Launches China's First 500,000-Ton Biomass Green Methanol/Ethanol Project
Weekly Insights
Stay ahead with our curated technology reports delivered every Monday.